CYVIATION, a cybersecurity company purpose-built for aviation, recently announced its strategic partnership with Boeing on the company’s newly launched SkyGuard service, deepening a relationship that brings continuous, aircraft cyber risk visibility to airlines, business aviation operators, MROs and OEMs worldwide.
As part of the strategic partnership, Boeing’s Aviation Business Solutions (ABS) Cybersecurity and Digital Practice will offer customers CYVIATION’s SkyRay platform through SkyGuard, delivering continuous compliance and risk assessment capabilities built on proprietary tail-specific digital twin technology that models each aircraft’s exact systems, devices, and connectivity. SkyRay generates audit-ready evidence aligned with FAA, EASA Part-IS, and other regulatory frameworks, runs entirely non-intrusively, and has no impact on airworthiness or daily operations.
The launch arrives as regulators tighten cybersecurity standards across aviation, including the FAA’s proposed rulemaking on Intentional Unauthorized Electronic Interactions (IUEI) and EASA Part-IS, pushing operators toward continuous, evidence-based cyber risk management.
“Operators are showing a strong interest in improving cyber resiliency with compliance-ready solutions,” said Eliran Almog, CEO of CYVIATION. “Partnering with Boeing on SkyGuard is a major milestone in our strategic relationship. Customers gain the continuous digital visibility that regulators are increasingly demanding — fleet-wide, tail-by-tail, without ever touching the aircraft. Our mission has always been to make the skies safer, and SkyGuard puts that capability directly in the hands of the operators who need it most.”
“Aircraft are now deeply connected systems, and our clients are asking for practical, evidence-based ways to manage cyber risk across their fleets,” said Tim Sikora, cybersecurity and digital practice principal at Boeing. “SkyGuard brings together Boeing’s deep aircraft expertise with best-in-class strategic partners like CYVIATION. SkyRay gives operators continuous governance and compliance readiness without touching the physical aircraft or impacting airworthiness, exactly the combination the industry needs as regulators raise the bar.”
CYVIATION and Boeing Aviation Business Solutions first announced their collaboration in October 2025. The SkyGuard strategic partnership formalizes and expands that work, positioning SkyRay as a dedicated compliance infrastructure layer available to ABS’s global customer base.
Lufthansa Technik Philippines, the joint venture between Lufthansa Technik and the MacroAsia Corporation, is significantly expanding its footprint in the Philippines with a new base maintenance facility at Clark International Airport. The announcement was made today during the state visit of German Federal President Frank-Walter Steinmeier, who met with Philippine President Ferdinand R. Marcos Jr. at Malacañan Palace in Manila. Both heads of state acknowledged the project as a milestone in German-Philippine economic cooperation.
The new site will span 157,000 square meters and is intended to offer capacity for up to nine widebody aircraft bays. Over the coming years, the three-digit million-dollar investment will create around 1,200 highly skilled jobs. First operations are scheduled to commence in 2028. The facility in Clark will be Lufthansa Technik’s second location in the Philippines and will complement operations at the long-standing site at Ninoy Aquino International Airport in Manila, where the company has been present for more than 25 years and recently secured a long-term lease extension. Together, both locations will form a powerful hub for widebody aircraft MRO (maintenance, repair and overhaul) and strengthen Lufthansa Technik’s presence in the Asia-Pacific region.
German Federal President Frank-Walter Steinmeier, together with Philippine President Ferdinand R. Marcos Jr., commended the project at Malacañan Palace during his state visit to the Philippines today, before touring the Lufthansa Technik Philippines facility in Manila.
Soeren Stark, CEO of Lufthansa Technik, who welcomed German Federal President Steinmeier at Lufthansa Technik Philippines, stated: “Asia-Pacific is one of the fastest-growing aviation markets in the world, and the Philippines are central to our strategy in this region. With the investment in the new site in Clark, we are taking the next decisive step in our growth strategy and positioning Lufthansa Technik for the future of aviation — well beyond the borders of this region.”
Holger Beck, CEO of Lufthansa Technik Philippines, said during German Federal President Steinmeier’s facility visit: “With the new base maintenance location in Clark, we are making a significant investment in the Philippines and substantially expanding Lufthansa Technik’s network in the country and across the Asia-Pacific region. Our sites in Manila and Clark will complement each other as two strong pillars of our growth, and together they mark an exciting new chapter for Lufthansa Technik Philippines. It is an honor that President Marcos Jr. and Federal President Steinmeier recognized this commitment during their meeting today. Welcoming Federal President Steinmeier to our facility in Manila is a particular pleasure, as he could experience firsthand the exceptional work of our highly skilled aviation experts.”
The expansion of Lufthansa Technik Philippines underscores the long-term commitment of Lufthansa Technik, the world’s leading provider of technical aircraft services, to the Philippines as a strategic hub. With both facilities, the company is well positioned to meet growing demand from its airline customers across Asia, Australia, Europe and the Middle East. As Lufthansa Technik’s competence center for widebody aircraft within its worldwide network, Lufthansa Technik Philippines specializes in the MRO of Airbus A330, A340, A350 and A380 as well as Boeing 777 aircraft. With the additional Clark facility, the company’s portfolio will also include the Boeing 787.
For eight decades, the American Airlines base maintenance facility in Tulsa, Oklahoma (Tech Ops – Tulsa), has stood at the center of the airline’s technical operations, evolving into the world’s largest commercial aircraft maintenance base and a cornerstone of the airline’s commitment to safety and reliability.
“American is proud to celebrate Tech Ops – Tulsa, a cornerstone of our aircraft maintenance operation,” said Kevin Brickner, senior vice president of technical operations. “Our team of skilled aviation maintenance professionals — in Tulsa and across our system — is the best in the business, and they set the standard for safety, quality and ingenuity. We wouldn’t be where we are today without our team members, the City of Tulsa and the State of Oklahoma. We’re eagerly looking forward to the next 80 years in Tulsa and beyond.”
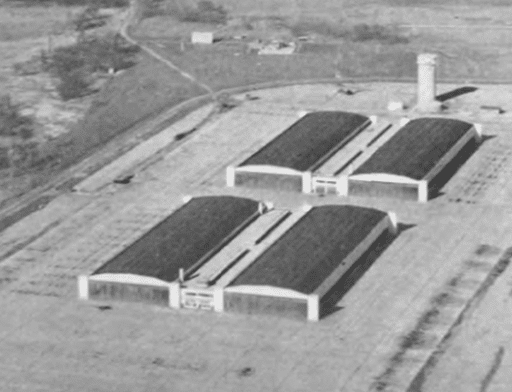
It all started in 1945 when the U.S. government listed a military aircraft plant as surplus property. The property, with four large hangars anchoring more than 260 acres, caught the eye of American’s leaders who soon negotiated a lease with the City of Tulsa and began relocating its maintenance and engineering operations from New York’s La Guardia airport to the new Tulsa facility. The move reflected American’s growth and Tulsa’s emergence as a major aviation and aerospace hub, bolstered by a skilled local workforce, which still holds true today.
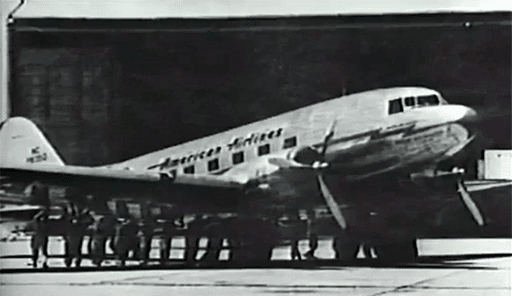
The maintenance base opened in June 1946 and started overhauling Douglas DC-3 aircraft. American’s then CEO and industry pioneer Cyrus Rowlett “C.R.” Smith celebrated the facility’s opening with an eye toward the future.
“We plan to become citizens of Tulsa and Oklahoma,” Smith said. “We plan a great expansion and development in this city and this state. Our future is ahead of us. We are looking forward.”
Over the years, almost every aircraft type flown by American passed through Tulsa’s hangars. Early propeller-powered models such as the DC-3 and Convair 240 soon made way for turbofan engines powering Boeing 707s. Boeing 727s and 747s and the McDonnell-Douglas DC-10s and legendary MD-80s later occupied hangars. Modern Boeing 737 and 787 families of aircraft touch down at the base for scheduled maintenance work today.
Tech Ops – Tulsa, which is currently undergoing $400 million in improvements, has grown to 3.3 million square feet of hangar and shop space sprawling across 330 acres at Tulsa International Airport. Together with the airline’s nearby offsite composite repair and wheel and brake facilities, these technical centers of excellence provide maintenance and related support to more than 400 aircraft that visit the base annually.
The source of the base’s success — and the standard set for the industry — is the people. Today, nearly 5,000 team members (including more than 2,300 licensed aviation maintenance technicians) work in aircraft overhaul, component repair, engine overhaul, engineering, supply chain, facilities maintenance and information technology, to keep Tech Ops – Tulsa moving 24/7. And they’re not just individual team members — the base has familial roots with generations of families working at the base over the decades.
Eighty years after the maintenance base opened, the airline continues looking forward to welcoming the next generation of aviation maintenance professionals through its hangar doors. In 2024, American announced a partnership with Tulsa Tech — the alma mater of many current Tech Ops – Tulsa Team members — providing interviews to top students and ongoing engagement opportunities with the airline’s team members, formalizing a decades-long relationship with the school. American also sponsored Tulsa Tech’s adult student team at the 2026 Aerospace Maintenance Council Competition. Tech Ops – Tulsa team members mentored students leading up to the competition, and that partnership paid off — the team took first place among all 47 schools.
Boeing announced a key milestone in its ongoing journey to modernize and integrate its distribution businesses with the launch of a new, unified ecommerce website. The new platform brings together Boeing Distribution’s portfolio of products and services into one streamlined digital destination, simplifying how customers and suppliers connect, transact and grow with the company.
Over the past year, Boeing Distribution has implemented several key initiatives to strengthen operations and elevate the customer experience. These include enhanced AOG access for faster response times, an improved customer support model that streamlines communication and resolution, and implementation of a new state-of-the-art enterprise resource planning system to unify data, improve visibility and support more efficient service.
“We want to simplify distribution services, maximize customer performance and be the preferred choice for customers and suppliers in the global distribution marketplace,“ said William Ampofo, senior vice president, parts & distribution and supply chain, Boeing Global Services. “The new ecommerce website — along with system and service enhancements — represents a significant step forward in that vision. Together, these investments strengthen our foundation and position us for continued growth.“
The new Boeing Distribution ecommerce website offers full product catalog and services offerings for commercial, business and general aviation, vertical lift and defense customers; smart search, powered by AI, to help customers find products faster and one single login.
MRO operations generate a significant amount of waste on a daily basis. This waste includes everything from solvents, degreasers, and chemical cleaners to composite scrap and removed parts, plus leftover hydraulic fluid, oil, and fuel residues.
Fortunately, many MROs are aware of this problem and are taking steps to reduce their environmental impact. Aviation Maintenance magazine spoke to four MROs who are doing their best to “go green.”
What They Are Doing
Montreal-based MRO AJW Technique takes sustainability seriously. To do so, the company has aligned its operations with the United Nations Global Compact by actively reducing its energy consumption, water usage, and general waste. AJW Technique also operates as an aviation recycling plant, continuously repairing and overhauling aircraft components to extend their lifecycle and prevent landfill buildup.
Louis-Philippe Mallette AJW Technique
“To minimize chemical waste from cleaning and degreasing processes, we prioritize aqueous solutions wherever possible,” said Louis-Philippe Mallette, president of AJW Technique. “In cases where performance requirements necessitate the use of solvent-based cleaners, we extend solution life through regular monitoring, filtration and controlled chemical top-ups. When replacement is required, waste is managed by accredited disposal partners who ensure correct identification, segregation, recycling, and safe disposal. A similar approach is applied to fluids used in our test stands, such as Skydrol and fuel. Through filtration, routine condition monitoring and, where necessary, water separation, we maximize fluid longevity and reduce waste.”
Most of the scrap parts generated by AJW Technique are metallic in nature. They are managed by specialist contractors to ensure proper segregation and recycling. “In addition, we have significantly reduced packaging waste by replacing expanding foam with paper-based cushioning and void fill systems,” Mallette told Aviation Maintenance. “These alternatives have a substantially lower environmental impact and are fully recyclable.
Headquartered in Munich, Germany, MTU Aero Engines drives sustainability through its group-wide ecoRoadmap program, which is focused on improving energy efficiency, adopting renewable energy, and electrifying systems across its sites. In alignment with the Paris Agreement, the company’s climate transition plan sets measurable decarbonization goals while pursuing a “circular economy” (closed-loop) approach from procurement to waste management.
“MTU addresses waste reduction in MRO through a combination of certified environmental management systems, site governance and a broader push toward circularity.
Alexander Engel MTU Aero Engines
Environmental management and compliance structures,” said Alexander Engel, MTU Aero Engines’ vice president for corporate sustainability management and reporting. “At MTU Maintenance Hannover, environmental protection activities explicitly include cooperation with environmental stakeholders such as a waste management officer, regular operational inspections, audits and KPI management. Such mechanisms are typically used to reduce waste generation and ensure proper handling of hazardous materials and residues.”
“MTU’s sustainability framework highlights circularity and a planned circular economy strategy,” he added. “It explicitly lists reducing raw material and energy consumption via ‘used parts management’ and industrializing repairs, which also reduces scrap and material throughput.”
Singapore’s ST Engineering is relying on technological solutions to reduce its environmental footprint, such as implementing its water-saving EcoPower engine wash system and utilizing additive manufacturing to produce lighter parts. The company also develops advanced nacelles to lower fuel consumption and has been integrating solar energy at its aerospace facilities since 2018.
“In component MRO, a wheel cleaning automation solution reduces the consumption of cleaning chemicals by up to 40%, while enabling overnight operations,” said an ST Engineering spokesperson. “When it comes to paint stripping, an automated media blasting solution eliminates the need to soak components in paint-stripping chemicals, which is part of a process that normally takes up to two days and entails heavy chemical usage.”
ST Engineering deploys a fully automatic and enclosed ultrasonic cleaning system for cleaning engine parts, which improves productivity while minimizing technicians’ exposure to chemicals. “Compared to the process of manually immersing parts in a large cleaning tank, this system uses smaller tanks with less liquid, meaning that less energy is consumed for heating, while the use of ultrasound technology provides better cleaning quality,” the spokesperson said. “Meanwhile, the use of extremely pure deionized water in our EcoPower aircraft engine wash system as a highly effective cleaning agent eliminates both the need for detergent and the risk of engine contamination.”
Headquartered in Scottsdale, Arizona, StandardAero is reducing its greenhouse gas emissions, energy use, and waste through its GreenERmro continuous-improvement program and a targeted decarbonization roadmap. StandardAero is aiming to achieve net-zero emissions by 2050 by scaling up its use of renewable energy, deploying electric ground support equipment, and optimizing resource efficiency across its operations.
Brian Skrobarcek StandardAero
“In 2025, StandardAero launched 85 GreenERmro projects that target energy, water, and waste reduction,” said Brian Skrobarcek, the company’s enterprise vice president for environment, health, safety & sustainability. As an example, “StandardAero’s Kansas City facility moved to a reusable grit‑blast medium, eliminating about 40,000 lbs of waste a year, with a 75% reclamation target.” Meanwhile, StandardAero’s Maryville facility found an alternative part‑cleaning process that avoids the use of about 28,000 gallons of water. The company’s Winnipeg facility has installed an efficient vacuum furnace with closed‑loop cooling, reducing energy and process waste.
In the area of recycling and circular approaches, StandardAero’s San Antonio facility is repurposing surplus equipment and converting materials into recyclable scrap, with 16% of its overall total waste being recycled in 2025. The company’s Fleetlands facility in the United Kingdom has initiated organic waste segregation and composting.
“Globally, our e‑waste is recycled or dispositioned appropriately,” Skrobarcek said. Additionally, “StandardAero’s Supplier Code of Conduct and procurement practices emphasize environmental stewardship, responsible sourcing, and proper handling of specialty materials.”
ST Engineering has implemented a water-saving engine wash system called EcoPower. ST Engineering image.
More Repairs, Less Replacements
In their efforts to go green, many MROs are repairing, overhauling, or remanufacturing parts rather than replacing them. “The first step is to confirm the part needs to be or can be repaired,” said Mallette. “If we are repairing rather than overhauling a component, we check whether all bearings and seals are still functional or whether they need replacing. Provided they are still within specification, there is no need to replace them. Our skilled engineers are equipped to identify opportunities to repair rather than replace them with new items. We also collaborate with partners who specialize in parts restoration processes such as plating and welding.”
AJW Technique’s approach is endorsed by MTU Aero Engines. “One of MTU’s core philosophies is repairing instead of replacing as a way to make our MRO operations more sustainable and more reliable,” Engel said. “We work closely with engine OEMs to develop, license and industrialize approved repair methods so they can be performed at scale. This reduces overall demand for raw materials and related energy consumption, as well as dependence on the market, while extending component life and maintaining airworthiness requirements. We also have a global network of Centers of Excellence that specialize in different areas of parts repair and help our MRO network conduct upwards of 90 percent of necessary repairs ‘in-house’.”
StandardAero explicitly prioritizes repair over replacement to extend component and engine life and avoid manufacturing‑intensive impacts. Mindful that time is money, “We use data analytics and predictive maintenance products such as EHM, ECTM, and Maintenance Insight to optimize time‑on‑wing and reduce unnecessary shop visits,” said Skrobarcek.
At the same time, “Certification and traceability are critical in aviation and can limit reuse/repair if documentation, quality controls, or provenance aren’t maintained,” he noted. To comply with these requirements, StandardAero employs rigorous quality management certifications, digitized record-keeping, OEM-authorized repair capabilities, and strict supplier oversight.
Making MRO Spaces Less Resource-Intensive
Because they service aircraft, MROs need large spaces to work in. These facilities consume substantial amounts of electricity, water, heating, and cooling resources.
So what are environmentally-conscious MROs doing to consume fewer resources? AJW Technique’s Montreal facility uses electrical power that is virtually 100% generated from renewable sources such as hydropower. “In all of our facilities we’ve moved to LED or low-power lighting systems to minimize energy usage, and in our Montreal facility we’ve installed an advanced control system on our multiple air extraction systems to ensure they only operate when required and at a flow level appropriate to the equipment in use,” said Mallette. “This has resulted in a 60% reduction in the volume of extracted air.”
In Singapore, ST Engineering has installed solar panels atop all its hangars and available building space to generate clean energy, fulfilling approximately one-third of its operational needs. Solar panel deployments are also being undertaken at its other facilities globally, while in Dresden, Germany, its joint venture Elbe Flugzeugwerke’s facility obtains all its electricity from renewable sources.
At MTU Aero Engines, “we employ a number of measures to drive down our CO2 footprint,” Engel said. “This includes heat exchangers and pumps as well as photovoltaic installations to electrify operations sustainably as much as possible. Smart lighting and optimization of ventilation systems at our locations also help reduce industrial energy consumption. At our Munich HQ, we have even built a geothermal plant that powers most of the site’s operations. A more recent development is the retrofit of MTU’s test cells to include sustainable aviation fuel (SAF) for performance tests.”
StandardAero has implemented several initiatives to reduce energy usage at its facilities. For instance, the company is electrifying its ground support equipment, such as replacing a gas tug with an electric model in Van Nuys and pursuing eTaxi certification with GTS to decrease aircraft taxi fuel consumption. By installing rooftop solar panels on its hangars, this MRO supplied nearly 25% of its Stockton site’s electricity needs in 2025 — and avoided over $99,000 in energy purchase from their local grid.
That’s not all. StandardAero saved over 170,000 liters of test-cell fuel in 2025 through a targeted efficiency process. The company has also installed smart controls, energy-efficient lighting, and WaterSense fixtures across its facilities, while improving energy performance and operational reliability at its San Antonio site by upgrading compressed air and chilled water infrastructure.
AJW Technique says it works closely with engine OEMs to develop, license and industrialize approved repair methods so they can be performed at scale. This reduces overall demand for raw materials and related energy consumption. The company has also installed solar panels. AJW image.
Preparing for SAF
Beyond reducing waste and facility emissions, many MROs are also preparing for broader industry fuel transitions, like Sustainable Aviation Fuel (SAF). “While SAF is ‘drop-in’, it still affects maintenance due to its different chemical composition that may affect seals, elastomers, and fuel system components over time,” said Skrobarcek. “It also has cleaner burn characteristics that may lead to different inspection intervals, plus fuel storage and handling differences at MRO facilities.”
They’re not alone. “MTU is preparing for SAF both at the test and infrastructure level, as well as through data and experience gathering,” said Engel. “We are already ready to test with SAF at our Hannover location and have successfully done so there with 100% SAF on a V2500 engine together with International Aero Engines (IAE). Because SAFs are still a fairly recent development in aviation, it is still to be seen how it affects engines in the long-term and over maintenance intervals.”on credit programs.
What Comes Next
Each of the MROs interviewed for this story have taken real and very tangible steps to make their operations green. So what are their plans to ‘go greener’, to improve upon the progress they have made to date?
At AJW Technique, “we continue to focus on repair development to minimize the purchase of new material and promote re-use and recycling across our global offices and operations wherever possible,” Mallette said.
Over at MTU Aero Engines, “we will continue to build on and further develop our sustainability initiatives and actions on a continuous basis,” echoed Engel. “Engine MRO is emerging as a key lever for advancing sustainability in aviation. Significant benefits can be achieved by extending engine service life through repair, reuse, and retrofitting. We can also enhance operational efficiency by leveraging data-driven, predictive maintenance as part of our engine fleet management services. When combined with circular economy principles, it is a boon to minimizing energy and material consumption. The full sustainability potential is realized when these approaches are consistently applied across the entire engine lifecycle.”
ST Engineering has installed solar panels atop all its hangars and available building space to generate clean energy, fulfilling approximately one-third of its operational needs. Solar panel deployments are also being undertaken at its other facilities globally. ST Engineering image.
To maximize solar energy generation, ST Engineering is exploring mobile solar panel deployments and is in the midst of designing and constructing a prototype unit. For its engine MRO business, ST Engineering is looking into implementing a carbon capture device to partially sequester greenhouse gas emissions from test cells, and has started to acquire blended SAF to drive down its direct greenhouse gas emissions.
As for StandardAero, the company is still following its goals of achieving 45% greenhouse gas reduction by 2030 and reaching net‑zero by 2050, finding additional energy-reduction efficiencies while using more renewable electricity, and electrifying more ground support equipment. The company also wants to further improve its test‑cell performance, form partnerships to increase the repairability of parts, and ensure that its suppliers are also doing their part to be more sustainable.
The takeaway is that these MROs aren’t just talking about going green; they are doing something about it. The result is a growing shift toward sustainability practices that are becoming increasingly integrated into modern MRO operations.
Counterfeit and fraudulently documented aircraft parts pose a direct safety threat to aviation maintenance, aircraft operators, and passengers. When detected after widespread usage, a poor-quality counterfeit bolt can ground an entire fleet. When undetected, it can cause a catastrophic mid-air failure.
Aviation Maintenance magazine recently sat down with two industry experts to discuss the threat of counterfeit and fraudulent aircraft parts, the vulnerabilities in today’s supply chain, and the technologies aiming to solve the problem.
Roei Ganzarski, Alitheon
Roei Ganzarski is CEO of Alitheon. His company utilizes patented optical AI technology to capture the inherent microscopic surface details of physical items, creating an unforgeable digital “fingerprint” that protects the aviation supply chain from counterfeit and fraudulent parts. “Our patented system, FeaturePrint, gives every physical item a unique digital identity — the equivalent of a fingerprint for things — using nothing more than a standard camera,” he said.
Jason Dickstein, MARPA
Jason Dickstein is president of the Modification and Replacement Parts Association (MARPA) and general counsel with the Aviation Suppliers Association. MARPA is a non-profit trade association representing manufacturers of FAA-approved aftermarket aircraft parts.
Aviation Maintenance: What are counterfeit aircraft parts? When we use the term, what are we referring to?
Roei Ganzarski: I would first like to expand this question to fraudulent parts, because the broader framing matters. Fraudulent parts include counterfeit parts, but also grey market parts.
Counterfeit parts, which are often called fake parts, are made to look like the original but are not actually produced by the original manufacturer. They are made with the intent of deceiving the buyer into believing they are receiving an original part. On the other hand, grey market parts are authentic parts made by the original manufacturer but sold illegally or against company policy. Examples include parts that have passed their certified shelf or service life and are resold with paperwork representing them as new, authentic parts that have been stolen, and quarantined parts placed back into circulation, whether intentionally or unintentionally.
The distinction and expansion are important because the industry conversation tends to fixate only on counterfeits — parts that are visibly fake — while grey market parts often pose an equal or greater risk. A counterfeit bolt may fail because it was never built to spec, but a grey market part can fail for subtler, harder-to-detect reasons. It may have exceeded its certified life, been exposed to conditions that compromised its integrity, been pulled from a scrapped aircraft, or been diverted from a use case it was never qualified for. The part itself is genuine, so traditional inspection, paperwork review, and even material analysis can all check out, yet the part is still unfit for service. In many cases, a grey market part might come with fake or manipulated paperwork, whether printed or digital.
A potentially useful way to understand the difference and the complexities that go with it is to think about identity fraud involving people rather than parts. A standard counterfeit part is like someone claiming to be me using a fake ID, where the document itself is forged. A stolen or diverted grey market part is like someone claiming to be me using my real ID. The credential is genuine and was issued by the real authority, but the person presenting it isn’t the person it belongs to. Every check on the document itself will pass, because the fraud lives in the gap between the credential and the individual holding it.
Alitheon’s FeaturePrint uses an optical AI technology to capture the inherent microscopic surface details of physical items, creating an unforgeable digital “fingerprint.” Alitheon image.
Then you have a grey market part that is authentic but the wrong individual, which is like my identical twin brother claiming to be me using his own real ID. He is exactly who his ID says he is, so the document is real, the person is real, and they match, but he is still not me. If you needed me specifically, accepting him would be a failure.
A sophisticated counterfeit paired with an authentic individual is like my identical twin brother claiming to be me using a high-quality fake ID. The document is forged, but well enough that cursory checks pass, and because the person looks like the individual named on the ID, even a careful human reviewer has nothing obvious to flag.
Finally, an authentic part with a falsified history is like my identical twin brother claiming to be me using my real ID. Now the deception is complete on every conventional axis. Document checks pass, visual inspection passes, and the only thing that fails is the one check almost no system performs: asking if this is the specific individual the credential was issued to.
Traditional anti-counterfeiting is built to catch the first case, and most paperwork-based supply chain controls can catch the second. But the other cases defeat almost every layered defense except deep forensic examination of the document. Catching them requires the ability to verify the specific individual, not the category they belong to or the paperwork they present. That is the gap fraudulent parts exploit. From a detection standpoint, grey market parts are often the harder problem, because the adversary isn’t trying to imitate authenticity — they already have it.
Jason Dickstein: First, it’s important to recognize that a lot of people call bad parts of all sorts counterfeit when, in fact, counterfeit has a fairly specific meaning under the law.
Under the Lanham Act, if you have created something that causes confusion, deceit, or mistake by using a likeness, trademark, or other mark of someone else, then you have created a counterfeit and violated the trademark rights of the other party. So, if I build a part and I say it’s a Boeing part, but I built it and Boeing didn’t, that is counterfeiting. Similarly, if I build a part and I spell it B-O-W-I-N-G, that is likely to be a Lanham Act violation as well because it is confusingly similar to the name Boeing. Ultimately, the metric that gets used by the courts is whether there is a likelihood that you’re going to create confusion, deceit, or mistake as to relevant facts such as the source or nature of the part.
We saw a fairly dramatic drop-off in counterfeiting after the FAA implemented AC 00-56, the voluntary industry distributor accreditation program, which basically resulted in companies seeking a measure of traceability. Interestingly enough, we have seen situations like the AOG Technics case where it turned out at least some of the parts were stolen and they created fraudulent documentation. It seems they were passing off the parts as what the parts actually were, but they were just trying to inhibit the traceability in order to avoid anyone finding out that the parts were stolen. So, there you’ve got an issue where the parts weren’t necessarily counterfeit, but they were stolen and the documentation was fraudulent.
Aviation Maintenance: How serious is the counterfeit and fraudulent parts problem?
Roei Ganzarski: I believe this is very serious. Have hundreds of people died from this? Not that we know of. Do we need to wait for that to happen? I don’t think so, and I really hope not. There are many well-documented cases just from the last few years that show the scale of the issue.
The AOG Technics case involving CFM56 engine parts in the U.K. is the largest aviation parts fraud case of the decade. The sole director, Jose Alejandro Zamora Yrala, was sentenced to prison after selling approximately 60,000 aircraft engine parts accompanied by forged Authorized Release Certificates created on his home computer. These parts went into engines that power the Boeing 737NG and Airbus A320ceo families, affecting airlines including American, United, Delta, Southwest, TAP Air Portugal, Virgin Australia, Ryanair, and Ethiopian Airlines. The estimated cost to the industry exceeded $50 million.
In 2024, counterfeit titanium was discovered in Boeing 737 Max, 787 Dreamliner, and Airbus A220 aircraft built between 2019 and 2023. The material entered the supply chain through forged certificates of conformity from a Chinese supplier, and the fraud only came to light when Italian parts supplier Titanium International Group discovered small corrosion holes and questioned the paperwork. Also in 2024, executives at Sofly Aviation Services in the U.S. pleaded guilty to purchasing “as removed” aircraft parts and reselling them to Canadian airlines and a U.S. Department of Defense contractor using forged FAA Form 8130-3 and EASA Form 1 certificates.
We have also seen major issues with life-safety systems. In 2023, the FAA warned of counterfeit Rockwell Collins Traffic Collision Avoidance System transmitters being sold by a company in Moscow and distributed through U.S. brokers. The units had been physically altered with counterfeit outer housings and forged identification plates, and when tested by the FAA, they were entirely inoperable. On the military side, a man in Miami was sentenced to federal prison in 2024 for running a massive counterfeit-trafficking operation, importing tens of thousands of low-quality networking devices from China and Hong Kong, relabeling them as genuine Cisco products, and selling them for use in the support platforms of U.S. fighter jets.
Alitheon’s Roei Ganzarski says its product, FeaturePrint, gives every physical item a unique digital identity using a standard camera. Alitheon image.
Other cases include an Italian investigation into the disappearance of €17 million in military aircraft parts diverted through forged “out-of-use” certifications, and a Russian sanctions-evasion parts pipeline where airlines purchased at least $1.2 billion in aircraft parts through deliberately obscured supply chains. We even see general aviation affected, like the case where Southern Aero produced and sold articles for Franklin Aircraft Engines without FAA approval for over a decade. Additionally, EASA has issued multiple notifications regarding aircraft manufacturer identification data plates being reported missing or stolen from in-service Airbus aircraft. Each plate carries the unique identity of a specific airframe, and a stolen one could be affixed to another aircraft to fraudulently inherit that airframe’s
certified history.
Jason Dickstein: Anytime you’ve got someone committing parts fraud, they’re probably going to have fraudulent documentation. The good news is that, in the grand scheme of things, there is relatively little fraud. There’s not zero fraud, but the industry has gotten pretty good at detecting it.
I actually found myself helping the Nassau prosecutor’s office in New York investigate a case where they weren’t sure what to make of the paperwork, but they were pretty sure something was wrong. They sent over a copy by fax machine, and I happened to know some of the people who had signed the documents on a personal level. I called one of them up, gave him the work order number, and asked if he had provided the document to the company in question. He pulled up the work order and said it was absolutely incorrect. Using that method, I was able to figure out where there was a string of genuine documents and where the disconnect happened. Historically, that is exactly what quality assurance professionals in aviation do when something doesn’t feel right.
That is the beauty of the FAA’s AC 00-56 system; it requires companies to retain traceability documents, which allows quality professionals and government investigators to track backwards. We will never get rid of fraud completely because there are people who don’t understand enough about aviation to realize what protections we have in place, but authorities have developed fairly robust systems to catch these things.
Aviation Maintenance: How do counterfeit and fraudulent parts get into the supply chain?
Roei Ganzarski: Fraud succeeds because verification in aviation today is overwhelmingly about documents, not about parts. The supply chain inspects paperwork to confirm the part is what it claims to be, but the paperwork itself is the easiest thing to fake, alter, or steal. Whether the fraudster is forging a Form 1, forging a certificate of conformity, stripping out an out-of-use record, or counterfeiting an identification plate, every documented case is fundamentally a paperwork or proxy attack.
There are several structural vulnerabilities in aviation that make this possible. First, most fraud is caught reactively, usually when a part physically fails or visibly differs from expectations, not proactively at receipt. For example, AOG Technics ran for over four years before discovery, and the titanium fraud spanned four years of production. A maintenance organization receiving a part with an apparently valid release tag typically doesn’t contact the named issuer to verify. The exceptions, like the TAP Air Portugal technician who broke the AOG case, are exceptions precisely because that level of scrutiny isn’t standard.
Furthermore, a part may change hands four or five times between the manufacturer, authorized distributor, broker, MRO, and operator. Each handoff offers an opportunity to substitute documentation without anyone having visibility into the full history. EASA has explicitly noted that suppliers and brokers are not regulated the way manufacturers and maintenance organizations are, and AOG Technics existed entirely in that gap. Finally, post-pandemic parts shortages, sanctions, aging fleets with discontinued production lines, and high-priced parts all create environments where buyers are willing to accept parts whose provenance they can’t fully verify.
Jason Dickstein: When it happens, it’s very serious because any part that is not provably airworthy is a risk, and it’s the sort of risk that we don’t want to take in the aviation industry.
Aviation Maintenance: What impact do counterfeit parts have when they end up in aircraft?
Roei Ganzarski: The impacts are layered, and they cascade. Safety sits at the center and dominates the conversation. Fraudulent parts can kill people, as we saw in the 1989 Partnair Flight 394 crash where counterfeit bolts attaching the vertical stabilizer wore down progressively until the tail broke off in flight. Fraudulent parts compromise safety through premature or unpredictable failure, defeating safety systems like TCAS units, and compromising predictive maintenance data. When a part’s history is fabricated, every downstream maintenance decision is being made on false information. It also creates fleet-wide exposure, forcing emergency inspections and groundings across multiple continents.
When fraudulent parts are discovered, the immediate financial impact is severe. Emergency groundings can cost an airline $250,000 or more per day per aircraft in lost capacity. Replacement parts must be sourced urgently, and MRO providers must divert entire teams away from scheduled maintenance to trace part histories and perform destructive testing. The U.K. Serious Fraud Office estimated AOG Technics cost the industry approximately $50 to $53 million. A recent ProvenAir blog stated that a recent Reuters analysis estimated the global financial burden of counterfeit aviation parts exceeded $2 billion over three years.
The indirect financial costs often exceed the direct ones. Aircraft with incomplete or unverifiable maintenance records lose significant value during sales or lease returns. Lessors routinely refuse asset redelivery if back-to-birth documentation cannot be produced for every installed component, meaning a single suspect part can stall a multi-million-dollar transaction. There are also insurance complications, warranty voids, severe legal liability exposure, and massive productivity losses across the supply chain.
Beyond finances, aviation runs on trust, and a single fraud case damages trust at every layer, from passenger anxiety to media scrutiny. It triggers regulatory responses that create additional cost and complexity industry-wide. There are also ESG impacts, as premature parts failures increase fuel burn and disrupt end-of-life recycling, while counterfeit networks are frequently associated with organized crime and labor abuses. Finally, for military aviation, counterfeit components create operational readiness issues and strategic exposures, as counterfeit electronics can carry compromised firmware or hidden backdoors.
Jason Dickstein: The real serious cases of counterfeiting and fraud, luckily, are not frequent and are usually caught. That having been said, look at the recent massive theft in Spain. A dozen sea containers of parts that had been identified to be scrapped were intercepted by someone with credentials that made them seem like the target scrapping facility. It appears to be a highly organized criminal activity.
Any theories about who did this involve someone actually stealing those parts to use them. If they try to use those parts, they are going to have to create fraudulent documentation. They may be engaging in a Lanham Act violation if they claim parties have done overhauls on the parts. You’ve got parts that may be genuine, but they have been used to a point where they are no longer safe for further use, which is why they were scheduled for mutilation. That is the sort of thing that I personally find very scary.
On the spectrum of counterfeiting, you can have parts that are completely unapproved, made of the wrong materials, and untested by the FAA or EASA. A part like that could fail prematurely. If it is a trim part on an interior, it might not impact safe flight and landing, but if you’ve got an engine part or a landing gear part, the failure could be catastrophic.
Aviation Maintenance: Finally, what can be done to identify and track counterfeit parts? Do solutions such as blockchain and digital traceability help?
Roei Ganzarski: Before answering what works, it’s worth being honest about three technology categories currently being marketed that have fundamental limitations.
The dominant approach today relies on proxies, which means attaching something to the part like a QR code, barcode, RFID tag, or hologram. The fatal weakness is that every proxy is not the part itself. Anything that can be added to a part can also be removed from it, damaged, worn off, transferred to a different part, or faked outright.
The second category is machine learning. While powerful, it works at the class level, not the individual level. It can tell you with high confidence that an object is a CFM56 high-pressure turbine blade, but it cannot tell you that it is specifically serial number 7724-A.
The third category is blockchain. Blockchain is genuinely an excellent technology for creating tamper-resistant records of digital data, but it does absolutely nothing to verify the physical part itself. It relies entirely on whatever physical proxy connects the digital record to the physical object. A perfectly secured digital record of a lie is still a lie.
The same problem existed for human identity until relatively recently. ID cards and passports could be forged, and even with holograms, the document was just a proxy for the person. The solution was to stop verifying the proxy and start verifying the person through biometrics. Fingerprints and facial geometry work because they are not added to the person; they are inherent, unique, and cannot be transferred to someone else, unless you are a fan of Tom Cruise in Mission Impossible.
We built FeaturePrint because the aviation industry needs the same capability biometrics gave human identity verification. FeaturePrint uses machine-vision algorithms and a standard camera to capture and analyze the microscopic surface characteristics that every manufactured object inherently possesses. No two parts have identical surface micro-geometry, which is exactly why manufacturing tolerances exist.
We don’t add this signature to the part. We don’t engrave it or stamp it. It’s already there. We simply read what’s already there and convert it into a digital identity that can be verified later, anywhere, by anyone with a camera. This anchors the digital record to the physical object itself, so the cryptographic ledger and the physical reality cannot drift apart.
Jason Dickstein: Today we have robust inspection systems. We rely upon traceability, and people in the industry know each other well enough to feel comfortable calling each other when documentation doesn’t look right. At the MRO level, installers also have obligations under FAR 43.13 to examine the part and confirm that it will return the aircraft to a condition at least equal to its original condition.
As we move from what we are doing today to what we could be doing tomorrow, digital documentation schemes are receiving a lot of scrutiny. If you’ve got a serialized part, you have a blockchain representation of that serial number. Using a blockchain mechanism, there is essentially a record that is off the chain and hashed to create a digital map. The hash becomes a part of the blockchain record, and if the data changes maliciously, the hash tells you that the data is no longer reliable. Normal change mechanisms add an additional record to the blockchain saying the record has changed and providing a new hash, allowing for a full traceability record.
The industry is making progress in combating the counterfeit and fraudulent parts issue. The Aviation Suppliers Association is part of the Aviation Supply Chain Integrity Coalition. They are sharing ideas and progress on digital documentation. They are also active with the Maintenance Management Team, which includes the FAA, EASA, Transport Canada and ANAC Brazil. Those four authorities have examined their regulations to make sure they don’t inhibit the sharing of digital documentation.
The Chinese already have a system right now where you can add parts to the blockchain when they are removed from a registered aircraft by a CCAR 145 entity. Disassembly facilities and repair stations seem willing to do this. For manufacturers, it is such a big undertaking that it is a little bit scary, but Boeing is already working with digital 8130s and venturing into this space. There are multiple projects out there, including AeroXchange, GA Telesis with their Wilbur project, and BlockAero, which is actually doing the programming on the database for the Chinese government’s approach.
Jason Dickstein: I’ve talked rather lovingly about the blockchain approach, but the problem is that you need some way to uniquely identify the digital record to the physical part. When you have a serialized part, you can do that. However, there are an awful lot of unserialized parts in the system, and we don’t yet have a universally good way to link them to digital records.
One of the approaches being investigated is basically having a picture of the part to identify unique features or flaws. There are two problems you run into with that approach. One problem is that you have to be photographing and imaging the part from the exact same angle, or else it looks different. Another problem is that the resolution of the cameras has to be sufficient to identify differences that may be measured in the thousandth or ten-thousandth of an inch, which makes it a somewhat expensive approach. Still, companies are investigating ways to make that work under current technologies. If you look at what was stolen in Spain, roughly 90 percent of the stolen parts were unserialized, which highlights why we need a way to digitally identify them.
All this being said, we are making progress as an industry. The Aviation Suppliers Association is part of the Aviation Supply Chain Integrity Coalition, where we are sharing ideas and progress on digital documentation. We are also active with the Maintenance Management Team, which includes the FAA, EASA, Transport Canada, and ANAC Brazil. Those four authorities have examined their regulations to make sure they don’t inhibit the sharing of digital documentation, and the next step is to do a similar project with guidance materials. We recognize that digital documentation is going to be the future, and we are trying to make sure that the regulatory authorities are prepared to support that.
Additive manufacturing has moved from a tool for prototypes and shop aids to a process applied, in defined circumstances, to actual hardware. For MRO organizations, the appeal is straightforward: components that are no longer procurable can be regenerated, and damaged metal surfaces can be restored with localized material addition rather than full replacement. What is perhaps less immediate is everything that has to happen before such a part or repair is released to service.
Processes such as selective laser sintering (SLS) and fused deposition modeling (FDM) have found a working niche in cabin component regeneration, where criticality is low to medium and dimensional tolerances are manageable with post-process finishing. Metallic processes, principally directed energy deposition (DED) and cold spray, are being evaluated for structural and heat-sensitive applications but remain considerably harder to qualify, particularly for the substrate adhesion, repeatability and mechanical performance data a design organization must produce.
The qualification requirements are the subject of sustained industry guidance. The Aerospace Industries Association’s (AIA) Additive Manufacturing Working Group has published two documents of direct relevance: “Recommended Guidance for Certification of AM Components” and “Considerations for the Use of Additive Manufacturing in the MRO Space.” Both are referenced throughout this article alongside operator accounts. This article illustrates how organizations are currently applying additive processes, how they test and qualify the resulting parts, what AIA’s guidance says about durability behavior and anomaly classification specific to AM, and how the regulatory chain from type certificate holder to repair station constrains what gets approved.
This chart shows the difference between two of the most commonly used additive manufacturing technologies in aerospace: selective laser sintering (SLS) and fused deposition modeling (FDM). TPM3D Printing Technology chart.
Additive Repair in Active MRO Environments
At Air France Industries KLM Engineering & Maintenance (AFI KLM E&M), additive manufacturing is currently used primarily to produce replacement components for original ones and to support cabin modifications, according to Jean-Baptiste Le Bideau, components industrial development director at AFI KLM E&M. “One example is the production of new power supply spacers with the same shape, size, and functionality as the original components. We also use 3D printing for repairs; however, in our case, this involves producing replacement components within equipment, rather than directly repairing the original component,” he says. “A good example is the creation of new components for the cabin crew communication system. The technologies we currently use are primarily selective laser sintering (SLS) and fused deposition modeling (FDM).”
FDM and SLS are two distinct 3D printing technologies. FDM extrudes melted plastic filament layer-by-layer, making it highly accessible and cost effective. SLS uses a high-powered laser to sinter powdered polymers, producing robust, complex and isotropic parts without support structures.
For Delta TechOps, additive repair represents a significant advancement in aircraft maintenance. “We see it as a proven approach to improving durability, efficiency, and sustainability, guided by rigorous engineering, safety, and certification standards, rather than focusing on individual component details,” a spokesperson says. “Delta TechOps is represented in the engineering and additive manufacturing fields on the Aerospace Industries Association’s (AIA) Additive Advisory Panel. Additionally, we contributed to and influenced the drafting of guidance documents on additive manufacturing in the MRO industry.”
Among the various additive manufacturing processes currently available, AFI KLM E&M has identified several ones that could potentially be used for repair applications within its maintenance activities, Le Bideau points out. “Some are specifically designed for the remanufacturing of complete components, such as SLS and FDM, while others are more suited to repair applications that involve material accumulation or deposition, such as directed energy deposition (DED) and cold spray. These processes differ from traditional repair methods, such as welding, in that they allow for highly localized material addition and, in the case of cold spray, without melting the material,” he says. “This could make them particularly relevant for our aluminum components, where heat input must be limited to avoid deformation. However, these processes are complex to implement, especially from a component qualification perspective.”
AFI KLM E&M is currently increasingly using SLS and FDM, both to regenerate certain damaged and non-repairable equipment parts and to manufacture alternatives to original equipment manufacturer (OEM) components. “Dimensional accuracy depends on the process used and generally requires additional finishing. One example is the cabin crew telephone unit, which is regenerated using FDM technology because the original component is non-repairable. These telephone units are then painted in different colors to match the interiors of customer cabins,” affirms Le Bideau.
Delta TechOps says they rely on advanced testing techniques and non-destructive evaluations to ensure reliability and consistency.
Testing in Additive Aircraft Repairs
Currently, Air France focuses exclusively on cabin components with low or medium criticality levels, explains Damien Jarriault, ALM team project manager of the innovation department. “This means that fatigue resistance is one of the criteria we consider, but it is not the primary factor guiding component design. When required by regulations, we perform mechanical tests in accordance with test plans issued by the design organization approval (DOA) holder and validated by a compliance verification engineer (CVE) to confirm the mechanical integrity of the parts,” he says.
All additive repair methods and applications are rigorously qualified to meet, and in many cases exceed, established performance and inspection standards, according to Delta TechOps. “We rely on advanced testing techniques and non-destructive evaluations to ensure reliability and consistency, although we cannot share detailed technical comparisons,” the spokesperson says. “We have collaborated extensively with a materials scientist at the Massachusetts Institute of Technology (MIT) on post-processing methods for components manufactured using laser powder bed fusion (LPBF) technology to match the properties of fused single-crystal components.”
Durability and Damage Tolerance
AIA’s report entitled “Recommended Guidance for Certification of AM Components” observes that durability and damage tolerance datasets can support a variety of end uses, economic needs for reliability, or individual design applicant design philosophy, and may influence the scope and type of data package developed. “Durability reflects a broader sustainment perspective that includes not only fatigue cracking but also corrosion, wear, and long-term reliability and service life considerations. Design data used in durability and damage tolerance analysis may be derived using a variety of industry or proprietary standard procedures with associated scale factors,” the report states.
From precise plastic adaptation to high-strength metal pressing tools, additive manufacturing offers numerous possibilities. Lufthansa Technik’s Additive Manufacturing Center focuses on repairing, replacing and developing new parts. Lufthansa Technik image.
Durability and damage tolerance properties are prone to a high degree of variability, and, because of this, methods of analysis must account for scale and scatter, points out AIA. “The characterization of additively manufactured components may differ from that of conventional products. These differences should be considered before assuming that traditional product behaviors apply and must be understood by the design applicant,” the report illustrates. “The durability and damage tolerance datasets must account for the components in the as used condition after all manufacturing, assembly and installation process steps.”
AIA affirms that difference in AM features and artifacts that should be considered include such aspects as microstructure, geometric features, defect morphology and their distribution. Additional features include surface roughness, morphology, and variation as built and/or final component surface, inherent process anomalies, residual stress distribution and mitigation strategies, performance of chemical post processing and coatings, post printing chemistry, post processing impacts (support removal and powdering techniques, and component extraction) and thermal exposure history throughout the build.
“These features and artifacts unique to additive manufacturing may impact the following aspects of durability and damage tolerance analysis; corrosion, stress corrosion, wear and tribology, corrosion fatigue, stress fields, stress level and stress ratio effects, susceptibility to embrittlement, starting flaw size assumptions, multi-site damage scenarios, cracking patterns, crack growth rate and interaction, inspection type and capability, multimode behavior, scatter, time to initiation, damage coalescence, and microstructural mechanics failure. This list is non-exhaustive and will be subject to the verification and validation of the design applicant,” AIA states.
Anomalies and Defects
Components made using additive manufacturing may exhibit certain internal or surface features that are anomalous compared to the basic structure, according to AIA in the ‘Recommended Guidance for Certification of AM Components’ report. “These features are an artifact of the manufacturing processes. The part requirements shall define acceptable limits for each of these anomalies and be documented in the type design and assured through the build quality plan. Only when these thresholds are exceeded is the anomaly then characterized as a defect and shall be submitted to the material review board (MRB).”
Some examples of material anomalies in additive manufacturing include porosity, i.e., the entrapment of small gas bubbles, common in metal solidification processes. Another anomaly is inclusion, which is a small particle chemically different from that allowed by the specification, according to AIA. “Lack of fusion is a condition in which fusion is incomplete, resulting in a lack of homogeneity in the resulting material. Lack of fusion can happen in both powder and wire deposition processes,” says AIA. “Balling is the instability of the molten material in the melt pool resulting in solidified spherical droplets on the build layer. This artifact can promote increased porosity and inclusions in subsequent layers.”
GKN Aerospace says it has one of the world’s largest additive manufacturing cells and dedicated centers in Trollhättan, Bristol, and Fort Worth. Their AM hubs are beacons of progress in additive manufacturing research and development enabling the production of large-scale aerostructures. GKN image.
Regulatory Pathway and Qualified Additive Repairs
Delta TechOps points out that additive repair is also conducted within a highly regulated framework, with oversight from authorities such as FAA and EASA. “Our approach prioritizes full compliance with these regulatory requirements, coupled with ongoing investment in our processes, facilities, and personnel to ensure safety and quality. The FAA also has a representative on the AIA working group for additive manufacturing,” the spokesperson says. “We collaborated closely with them, along with other industry experts in developing the AIA documentation on Additive Manufacturing in MRO.”
Le Bideau observes that there is no true generic approval applicable to MROs for qualifying an additive repair process. “In practice, a design organization must qualify the additive manufacturing process to be used — for example, DED or Cold Spray — and then design and approve the repair to be applied to the equipment in question. The repair is then performed by a Part-145-certified shop,” he says.
To evaluate the use of additive manufacturing in the aftermarket, it is necessary to understand the relationship between the original equipment manufacturer (OEM) and/or design approval holders (DAH), air carriers, and MRO organizations, AIA observes in a document entitled “Considerations for the Use of Additive Manufacturing in the MRO Space.” “The OEM/DAH designs a product and applies for a type certificate (TC); once the TC is approved and issued by the FAA, the OEM is referred to as a TC holder. The TC holder must establish a set of instructions for continuing airworthiness (ICA); this data is often, but not exclusively, published in maintenance manuals and provided to the air carrier,” explains AIA.
The air carrier is responsible for all maintenance performed on an aircraft and maintaining airworthiness. ICAs are an integral part of developing a continuous airworthiness maintenance program (CAMP), created pursuant to 14 CFR Part 135 or 121, explains AIA. “Under a CAMP program, air carriers may allow the use of designated engineering representative (DER) approved repairs and/or alterations to aid in maintaining airworthiness, creating an opportunity for the introduction of additively manufactured components and/or parts in the aftermarket. It is therefore imperative that the DER be cognizant of the process-sensitive nature of AM part manufacturing as outlined in the AIA ‘Recommended Guidance for Certification of AM Components’ document, EASA CM-S-008 Issue 3, and other emerging regulatory framework documents,” AIA affirms. “The repair shop (MRO facility) is required to adhere to all requirements of the CAMP. This includes having the OEM/DAH-generated ICA flow down to the repair station for execution of the maintenance or repair activity. The repair station may request and receive further information from the OEM/DAH through the air carrier or from the OEM/DAH directly.”
There are numerous limitations in qualifying these processes, some of which are beyond the capabilities of MRO companies, especially for metal parts, affirms Le Bideau. “Demonstrating and justifying the key parameters required for qualification, including repeatability, mechanical performance, and substrate adhesion quality, is extremely complex. This requires extensive testing and detailed analysis of parts with widely varying materials, geometries, and damage conditions,” he says. “An MRO can only produce parts that fall within the scope of its Part-145 certification. The manufacturing process itself must be validated through the organization’s quality assurance system. Aircraft components manufactured according to European parts approval (EPA) regulations, however, are produced by Part-21G certified manufacturers, which allows them to issue EASA Form 1 certificates.”
Artificial intelligence is increasingly being integrated in the aircraft MRO environment, and Delta TechOps is committed to promoting the use of data and analytics throughout the repair workflow, from inspection to return to service. “While AI supports our ability to anticipate needs and optimize processes, it is important to emphasize that AI provides insight, not a replacement, for expert human decision-making across all certified repair outcomes,” affirms the spokesperson.
The Emerging Picture
The picture that emerges from operator practice and industry guidance is that where criticality is bounded and the failure consequence is low, as with cabin equipment produced by SLS and FDM, additive repair has already moved into production use. Where criticality rises and the process involves fusion or deposition of metal, the qualification path lengthens considerably: substrate adhesion, residual stress, surface-connected porosity, and the directional dependence of material properties all have to be characterized before a design organization can sign off a repair, and that characterization work sits with the design approval holder rather than with the repair shop alone.
The regulatory architecture gives a clear structure to the division of responsibility, but it does not amount to a generic approval for additive processes. Each repair is qualified against the specific component, material, and damage condition at hand, drawing on instructions for continued airworthiness, CAMP provisions, and either FAA or EASA oversight depending on jurisdiction.
Artificial intelligence has a role in that effort, principally in inspection and process analytics, but for the time being it informs rather than replaces the engineering judgment on which certified return to service ultimately depends. For the wider MRO sector, the practical guidance is to match the technology to the criticality at hand, invest early in the inspection and material data that any qualification will demand, and use AIA’s published guidance as a working reference.
Hangars play a major role in aviation infrastructure. These dedicated structures designed to protect aircraft such as private planes, jets and helicopters are more than just storage buildings or utilitarian boxes. Hangars also provide space for maintenance, fueling, inspections and aircraft preparation before flight. They are carefully engineered aviation facilities that protect valuable aircraft, support maintenance operations and ensure safe daily aviation activity.
To make this happen, AI simulation software with space planning, bay scheduling and MRO capacity management can positively impact a hangar’s success and long-term performance. It can take into account crucial factors including door systems, clear span options, proper ventilation and adherence to building codes for optimal functionality and longevity. With the right software used correctly, aircraft hangar planning allows owners to build facilities that are safe, scalable and cost-efficient.
“One of the most overlooked assets in an MRO operation is the hangar itself,” says Matthew Curry, founder and CEO, Stax Aviation Group, Paso Robles, California. “Powered simulation allows operators to treat hangar capacity as a strategic resource by visualizing, testing and optimizing facility utilization before aircraft ever enter the building. In many cases, operators can increase throughput without adding square footage simply by making better planning decisions.”
AI Simulation Software and Hangars
Greg Lamp AirPlx
AI simulation software helps operators turn a complex hangar, ramp or maintenance schedule into a practical operating plan. Greg Lamp, CEO of Airplx in Boulder, Colorado, compares hangar planning to playing 3D Tetris on a calendar: teams need to know where each aircraft fits, when it fits, what has to move around it, and what happens when the schedule changes. “The software helps planners make faster, better decisions without replacing their operational judgment. It reduces manual work, improves team communication and helps operators make better use of the space they already have.”
Tom Torosian TruVideo
The aviation MRO industry has made tremendous strides in digitizing maintenance records and operational systems, but Tom Torosian, director of aviation business development at TruVideo in Wellesley, Massachusetts, explains a critical blind spot has remained: real-time visual context at the point of work. “Every minute an aircraft sits in a maintenance bay costs airlines money, and that occupied bay is a bay unavailable for the next aircraft in the queue. Poor communication between technicians, engineers and decision-makers compounds those delays, turning manageable repairs into extended hangar occupancy that cascades across an entire maintenance schedule.”
A video intelligence engine can fill this gap by embedding directly into MRO workflows as the visual layer when existing systems are missing. “AI-powered video enables technicians to instantly capture, annotate and share high-definition footage of maintenance findings — triggering faster diagnostics, sharper engineering decisions and dramatically reduced aircraft-on-ground (AOG) time,” Torosian says. “The faster an aircraft is accurately diagnosed and repaired, the faster it exits the bay, and the sooner that bay is available for the next aircraft. AI-powered video intelligence doesn’t just improve communication; it directly drives hangar throughput, bay utilization, and MRO capacity management in ways that scheduling software alone cannot achieve.”
Next-Generation, Purpose-Built
AI simulation software for hangars is still evolving but some MROs still implement hangar space planning and bay scheduling with tools and resources that really weren’t designed for it. Lamp explains that many operators are still using a mix of general-purpose tools: spreadsheets, whiteboards, Outlook calendars, Visio, Microsoft Paint, ERP/MRO schedules, and sometimes even cardboard cutouts. “Those tools are flexible … and track information …, but they are not built for aviation space planning. They do not understand physical space. An ERP schedule may know when work is due, but it usually cannot tell you where the aircraft should go, what else has to move, or whether the plan actually fits inside the hangar.”
Torosian agrees many MROs still rely on spreadsheets, whiteboards, and Outlook calendars to manage bay scheduling, many also depend on manual, paper-based inspection documentation and fragmented verbal communication between technicians and engineers. “The compounding effect of both is the same: aircraft stay in bays longer than necessary, hangar space gets locked up, and capacity planning becomes reactive rather than strategic.”
Curry explains that previous tools could track schedules and maintenance events, but they could not provide an accurate way to visualize, test and optimize how aircraft physically occupy and move through a facility. “Traditional scheduling systems are excellent at tracking work; they’re not designed to optimize physical space. The real opportunity lies in connecting operational schedules with spatial planning so that both time and space are managed together. Modern platforms create a digital representation of the hangar environment and allow operators to model aircraft movements, maintenance bay assignments, tow paths, clearance requirements, equipment staging areas and future maintenance schedules in real time.”
AirPlx’s purpose-built hangar and ramp planning software combines visual planning, aircraft geometry, scheduling, simulation and optimization in one place. Shown here is a digital twin of a real hangar with aircraft and visualizing customer SOPs. AirPlx image.
Next-generation, purpose-built hangar and ramp planning software like AirPlx combines visual planning, aircraft geometry, scheduling, simulation and optimization in one place. Lamp explains this gives MRO teams a visual, shared planning layer on top of the schedule. It helps them move faster, reduce manual rework and turn the plan into something the whole team can understand and execute. AirPlx creates a digital twin of the real hangar, ramp, aircraft and schedule. That gives AI and optimization tools the operational context they need to be useful, instead of asking a generic AI tool to guess how a hangar works.”
Sources at Lincoln, Nebraska-based Duncan Aviation explain that “AirPlx augments our team’s expertise by helping surface planning options, constraints, and fit considerations that are difficult to evaluate quickly with traditional tools.”
Advanced optimization engines can evaluate thousands of possible aircraft placement scenarios in seconds and recommend layouts that maximize space utilization while maintaining required safety margins. “Stax capabilities include capacity planning, fit analysis, conflict detection, scenario modeling and what-if simulations that allow MROs to evaluate future workloads before accepting additional aircraft,” Curry says. “Some platforms can also incorporate historical operational data to identify trends, improve forecasting accuracy, and help management make more informed decisions regarding staffing, facility utilization and growth planning.”
Curry cautions that one important distinction is that today’s hangar software planning tools are decision-support systems, not decision-makers. “Responsibility for operational safety, regulatory compliance, and maintenance execution remains with the operator. The value of Stax software lies in helping organizations consistently apply safety and operational standards while improving visibility into complex planning decisions. The system can help support compliance efforts by documenting aircraft positioning decisions, movement plans, and capacity assessments, creating a more auditable planning process.”
Video Intelligence Engine
A video intelligence engine can modernize the inspection and communication process without displacing the scheduling and ERP systems already in use; in fact, it actually enhances them. “Technicians capture structured, AI-tagged video documentation as a natural part of their workflow,” Torosian says. “Engineers receive real-time visual context and can make repair decisions remotely, eliminating the delays caused by waiting for the right expert to physically arrive at the aircraft. AI within the platform automatically organizes footage by aircraft, task, and finding — feeding structured visual data back into the maintenance workflow and creating a feedback loop that shortens repair cycles. The result is a meaningful reduction in the time each aircraft occupies a bay, which is the most direct lever available for improving hangar space utilization and MRO capacity. What starts as a workflow upgrade quickly becomes a measurable competitive advantage in throughput and bay availability.”
Modern video intelligence solutions leverage artificial intelligence to automatically detect anomalies and flag potential defects during inspections, turning passive footage into active diagnostic data. AI-driven object recognition can identify components, cross-reference known failure patterns, and surface relevant maintenance history in real time — giving technicians and engineers insights that previously required hours of manual review.
Torosian believes the downstream impact of all this on hangar space is direct and measurable: faster AI-assisted diagnostics mean shorter bay dwell times, fewer aircraft waiting for engineering approvals, and a more fluid, predictable flow of aircraft through the maintenance facility. “What video intelligence replaces is a fragmented, delay-prone system of verbal descriptions, handwritten notes, and static photographs that left engineers making critical decisions without the full visual picture — and aircraft sitting idle in bays they should have vacated hours earlier.”
Shown here is AirPlx’s AI making suggestions for where to position an aircraft. AirPlx image.
Other Factors
It is nearly impossible to not discuss the cloud when discussing today’s high-tech AI simulation software. The cloud makes hangar planning easier to share, update and use across the team. Instead of passing around files or relying on one local workstation, everyone can work from the same current plan. “It also reduces installation complexity and gives software providers more compute power behind the scenes,” Lamp says. “That matters for simulation and optimization, where the system may need to evaluate many possible planning options quickly.”
Do not forget about customization. Hangars are incredibly complex, especially in MRO environments. The aircraft is only one part of the planning problem; teams also have to account for tooling, equipment, work areas, restricted zones, doors, columns, and all the other real-world constraints inside the hangar.
Every hangar is unique. Curry explains that differences in building geometry, support columns, maintenance docks, office spaces, fire suppression systems, utility locations and door configurations can dramatically impact usable space. “The Stax platform addresses this by creating digital representations of each facility. Operators can model exact hangar dimensions and incorporate permanent infrastructure, restricted areas, maintenance bays, equipment storage locations and custom operating procedures. This customization allows simulations to reflect real-world conditions rather than idealized floor plans. The result is more accurate planning, improved operational confidence and safer aircraft movements.”
Stax capabilities include capacity planning, fit analysis, conflict detection, scenario modeling and what-if simulations that allow MROs to evaluate future workloads before accepting additional aircraft according to Stax CEO Matthew Curry. Stax image.
Lamp explains that up until now, “The most customizable tools were often general-purpose drawing tools like Visio or Microsoft Paint, but those tools were never designed for aviation planning. AirPlx has taken this problem seriously by building highly customizable hangar modeling into purpose-built planning software, so operators can model real-world complexity with aircraft, schedules, clearances and operational constraints all connected.”
Digital hangar simulation software allows MRO operators to visualize aircraft placement, maintenance bay assignments and movement plans before execution, helping maximize facility utilization while reducing operational risk. Image courtesy of Stax Aviation Group
For aviation maintenance facilities tasked with any refinishing function, the margin for error is razor-thin. A single misstep in surface prep, paint application or environmental control can trigger costly rework, delaying delivery schedules, straining labor resources and eating into profitability. These aren’t just technical setbacks — they’re operational liabilities.
Richard Giles Global Technical Service & Training Manager for Sherwin-Williams Aerospace Coatings
Facilities that consistently avoid extensive rework aren’t just lucky — they’re disciplined. They invest in proven coatings systems, enforce rigorous training protocols and understand the foundational causes of common paint failures. By getting back to basics, maintenance, repair and operations (MRO) teams can dramatically reduce rework incidents; protect their bottom line; and deliver flawless finishes on time, reinforcing customer trust.
Aircraft refinishing rework is the process of modifying or correcting the refinishing of an aircraft’s exterior to meet specifications. Rework to correct defects of a newly applied coating is inevitable and a crucial part of quality control.
It’s a common misconception that if the paint finish looks flawed, the paint itself must be the root cause. The coatings themselves are rarely the culprit. Most rework issues stem from process controls, whether in surface preparation, application technique, environmental or equipment condition. These foundational elements play a critical role in achieving a durable, high-quality finish and when they’re overlooked or inconsistently executed, the results can be costly.
So, in the grand scheme of things, what does it cost an aviation paint shop when it comes to rework? Plenty.
Aerospace coatings rework requires more than just additional materials. The biggest costs involve wasted time and increased labor. These are practically hidden among other operational inefficiencies, as rework and reactive maintenance issues aren’t factored into most paint job schedules and budgets. Rework can disrupt schedules, cause budget overruns, and increase stress among management and the workforce.
The need for rework can arise from various issues, such as:
• Surface contamination: Dust, dirt or other particles can become embedded in the paint during application, requiring a re-sanding and repainting of the affected area.
• Inconsistent paint application: Improper technique can lead to uneven application, known as “orange peel,” a wavy surface that must be sanded down and recoated, or over- or under-sprayed areas.
• Adhesion problems: If the paint does not properly adhere to the underlying surface or primer, it can flake or peel. This requires removing the paint and re-prepping the surface.
• Masking errors or bleed-through: Mistakes in painting stripes, logos or registration numbers require a precise re-masking and repainting of those sections or correcting where paint seeps under the masking tape.
• Cleanliness: Taking the time to clean the booth and aircraft thoroughly before the painting process starts can help avoid rework. That should be a part of a disciplined process, including regularly changing out paint booth filters, having strict entry protocols and scheduling deep cleaning.
• Minor damage: Small scratches or chips that occur during or after the refinishing process may need to be touched up.
Or … It Could Simply Be an Issue with the Paint Area Environment
Sometimes, even when all the hands-on processes are followed to the letter, Mother Nature steps in and causes an issue. The paint crew needs to be aware of, and deal with, the presence of unfavorable environmental conditions. Subsequently, a controlled environment is advantageous for a high-quality paint job.
Efficient and effective ventilation is an absolute must. Inadequate airflow in the paint booth or hangar can allow airborne dust and debris to contaminate the wet paint.
Refinishers need to be mindful of high humidity. Excessive moisture in the air can cause blushing, a cloudy or milky appearance caused by moisture trapped in the paint film. It can also slow drying time and increase the risk of paint runs.
There could be issues with improper temperature. Temperatures that are too hot, or too cold, can affect wet edge, dry times, and paint flow and levelling consistency.
And finally, there’s even static electricity. Static on a panel can attract dust and other airborne particles, leading to more contamination in the paint finish. Grounding of aircraft is essential.
Training Teaches and Reinforces Proper Techniques and Process Knowledge Why does rework occur?
It’s not done maliciously, but in the course of every aircraft paint job, errors can occur — even with the most seasoned painting teams. Often, the paint job is the final part of an aircraft’s MRO journey and there’s a rush to get back into the field and start making revenue for its owner or brand, especially if it’s a commercial plane that has been out of commission for weeks or months.
This can cause even established paint teams to skip steps, take minor shortcuts or overlook standard maintenance required to produce a flawless finish.
Proper training prevents aircraft refinishing rework by ensuring technicians have the knowledge, skills and discipline to complete the job right the first time. It minimizes common errors that lead to defects, enhances efficiency and ensures compliance with strict aviation safety standards.
When it comes to avoiding rework, following best practices is imperative. Adhering to established application guidelines can help prevent rework by ensuring the correct surface preparation, paint application techniques and post-paint inspection procedures.
Rework occurs due to a lack of training, limited shop resources and consistent mentoring in the paint shop. Thorough training courses (for both novice and seasoned refinishers) focus on the specifics of the aircraft refinishing process, allowing technicians to avoid common pitfalls and reinforcing best practices for every paint job:
• Surface preparation: Trainees learn to properly clean, strip, mask and sand surfaces to ensure optimal paint adhesion and a smooth finish. Without correct surface preparation, paint can peel, flake or fail prematurely.
• Corrosion prevention: Technicians are trained to identify, remove and treat corrosion before painting. Since improperly treated corrosion will grow under the new paint, this step is crucial for avoiding costly future repairs.
• Equipment use: Training covers the correct setup, operation and maintenance of specialized spray equipment. This ensures a uniform coating and avoids issues like improper thickness, which can lead to runs, drips or insufficient coverage.
• Application techniques: Proper training teaches the best methods for applying paint to the complex curves and surfaces of an aircraft. This minimizes defects such as “orange peel,” uneven layers and other visible flaws.
Human Factors and Error Reduction
Training addresses the human element of aircraft maintenance, which is a major contributor to rework and incidents. It also reinforces best practice adherence, which should reduce rework issues and minimize the mistakes. Regular and updated training assists in many ways:
• Attention to detail: Repetitive tasks can lead to complacency. Training emphasizes mindfulness and attention to detail during every step of the process to catch and correct mistakes early.
• Adherence to procedures: Aviation regulations require that all maintenance follow standardized, approved procedures. Training instills the discipline to follow these strict protocols without taking shortcuts.
• Identifying issues: A well-trained refinisher can quickly identify problems — such as dust inclusions, sagging paint or an uneven coating — and rectify them before a new layer is applied, which avoids more extensive rework later.
Operational Efficiency and Cost Savings
Investing in training is a proactive strategy that offers significant returns by avoiding unproductive labor activity and the high costs of rework. Better workforce and cost efficiencies include:
• Reduced downtime: Rework requires taking an aircraft out of service a second time. Getting it right the first time minimizes delays and gets the aircraft back into operation faster. It also assists in significant labor savings — the most expensive part of any aircraft repair or overall job.
• Lower material costs: Fixing a flawed paint job means using additional strippers, primers and topcoats. Proper training reduces wasted materials, contributing to cost savings.
• Increased throughput: When a team is highly skilled and consistently keeps rework to the absolute minimum, it can move on to new projects which increases the shop’s overall capacity.
• Enhanced reputation: A reputation for high-quality work and on-time delivery attracts more business and builds customer confidence.
Since aerospace coating technologies and regulations are always evolving, ongoing training is essential. Recurrent training with refresher courses ensures that technicians remain proficient and up to date with current best and repetitive practices. They can introduce and help refinishers become proficient with new technologies, as well as the latest products and application techniques. And in some cases, they can even provide certifications, which validate a technician’s or the whole team’s competence, offering assurance to employers and customers.
Why You Need to Avoid Rework
The rework process is time consuming, costly and frustrating to all involved. In addition to confirming each day’s paint shop assignment, paint teams should “huddle” every shift before performing tasks to assure all procedures are in place and followed.
As pointed out, consistency breeds good results. MRO maintenance directors and managers need to look closely for preventive maintenance savings and training opportunities to better produce consistent and quality work.
MRO directors of maintenance can learn more about the latest aerospace coatings products, service and training opportunities by contacting their Sherwin-Williams Aerospace representative or its product distributors in their area. To learn more, visit https://industrial.sherwin-williams.com/na/us/en/aerospace/contact-us.html.
ITS was founded in May 2002 and since that time the company says it has refocused its strategy. ITS made their first acquisition of a complete aircraft in 2007. With that experience, ITS’s leaders redirected the company’s focus to support the used serviceable material (USM) market and the global air transport industry. The company says this new strategy began with the MD-80 family and transformed ITS from a parts wholesaler into a global supply chain company. ITS began providing complex components and systems while developing in-house technical expertise on the entire airframe. Throughout the years, ITS has expanded the number of aircraft types they serve and has strategized with current and forecasted market demand to include support for various engines and APUs. ITS is headquartered in Chandler, Arizona, in a 100,000 sq. ft. state-of-the-art facility and holds ISO 9001:2015, AS9120B:2016, and ASA-100 accreditations. Aviation Maintenance spoke with Reid Selover, chief strategy officer to learn more about the company, its business philosophy and its goals.
Reid Selover
AVM: ITS has taken an interesting position in the supply chain arena. Tell us more about that and give us more background on the history of ITS.
Reid Selover: We just celebrated our 24th anniversary in the last couple of months. The company was founded by Ryan Kohnke and Scott Tinker, two college buddies who got into this space and the USM market. It is an interesting business. In a nutshell, ITS buys aircraft and helps airlines retire them so we support the remaining active fleet with critical USM components. Aircraft have a certain life expectancy, and at the end of that life, we acquire them and Dismantle them down to their critical components. We have those components returned to service and then sell them back to the airlines. That happens in a couple of different ways. In some scenarios, airlines consign the aircraft to us because they want to receive a little more return on their investment, and they trust ITS to help them do that. Much like a regular acquisition, we take over the aircraft, dismantle it, and manage the components and major pieces across the entire aircraft, from tip to tail. We then have those components returned to service. When we are helping an airline retire an aircraft, it may keep certain components or take some of them back. We may also sell the material into the market and share the value with the airline. That allows the airline to realize a little more from its investment.
AVM: What sets ITS apart from its competitors?
Selover: There is certainly competition in this space, but what sets us apart is our experience and technical know-how. We have torn down well over 300 aircraft, . There are not many companies with that level of experience and know-how. The other thing we do is work closely at the airlines we support. A major airline customer may operate one specific aircraft type or several different platforms. We look at the aircraft that are retiring and available, and we target the types that directly support those customers. We want to make sure we have a steady supply of material for them. Other companies may be more opportunistic. They acquire whichever aircraft becomes available, tear it down, sell the material, and may not know what the next aircraft will be. Some of our competition don’t even buy aircraft. They buy material from ITS or companies like ours and then flip them to the airlines. We are much more intentional about aligning our aircraft acquisitions and material with the platforms and customers we support.
AVM: What is ITS’s strategic mission?
Selover: We want to be the best nose to tail supply chain partner in the market. There is a lot of competition in this space, and you really have to fight for those aircraft. You have to position yourself well with the people who own the aircraft so you have the opportunity to buy them. You also have to do it intelligently so there is still value available for the airlines. That is where we are really strong. We call it “Win the Platform. Earn the Customer.” We do that through our relationships and through a concierge-style, white-glove approach to supporting our customers. We think these things through, look closely at what our customers need, and determine how we can best support them. That is where we perform well.
AVM: How do you determine what your customer’s needs are?
Selover: That’s where our experience comes in. Because we have been doing this for so long, we understand what fails and how often it fails. It comes from touching the parts, knowing what they are, understanding what they do, knowing where they live on the aircraft, and knowing how they work. And we Listen to our customers. To us, it is not just a part number on a page. We know what those parts look like, what they do, where they live, what other parts of the aircraft they affect, and what other systems they touch.
AVM: Give us an example.
Selover: A good example would be the flap carriages on a 747. You have a lot of metal sitting on these large, heavy aircraft, with components that are moving all the time and performing very specific functions that allow the aircraft to fly. We want our team members to understand what they are working with, what they are supporting, and how those components support the aircraft. That knowledge allows them to better educate and support their customers and their counterparts at the airlines.
AVM: You say ITS places a lot of importance on communications and training. Tell us more about that.
Selover: We want to be good communicators. I mentioned earlier that we provide white-glove service, and part of that is being able to clearly communicate exactly what we do and how we do it. Some of the training we bring in is specifically focused on communication. How should we speak to one another? How do different people listen to and receive information? What is important about the value proposition we are offering? When we tell our customers that we are going to take care of them, we want our team to understand exactly how we are going to do that and be able to communicate it clearly. We also want to help the customer understand how we are going to support them.
AVM: Is having the right team also important?
Selover: Having the right team is the Key to our success! We want our team to understand what our history is, our experience and our technical know-how so they can convey that to our customers. So, as I mentioned, we work on communication training. We work on teamwork. We rely on each other very heavily. This business doesn’t turn off. We are available 24 hours a day, seven days a week. There’s AOG support here and understand when you’ve got an aircraft on the ground you need to send parts counter-to-counter to keep that aircraft flying. And so, when the airline is at a work stoppage, you’ve got to know how to handle that. That’s really what the training is for us. It is who we are as an organization — what’s important to us. Internally we talk about our observable behaviors. This is what the best person is on the best day. We use those traits to hold ourselves accountable and to be better. The culture is a big, important thing for us and it’s something that we’re always going to work on. Even when you’re getting it right, you have to be involved in that all the time. You don’t turn that off either. It’s intentional. It’s an intentional culture.
We use cookies on our website to give you the most relevant experience by remembering your preferences and repeat visits. By clicking “Accept”, you consent to the use of ALL the cookies.
This website uses cookies to improve your experience while you navigate through the website. Out of these, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may affect your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. This category only includes cookies that ensures basic functionalities and security features of the website. These cookies do not store any personal information.
Functional cookies help to perform certain functionalities like sharing the content of the website on social media platforms, collect feedbacks, and other third-party features.
Performance cookies are used to understand and analyze the key performance indexes of the website which helps in delivering a better user experience for the visitors.
Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc.
Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads.